Open & closed die forgings · Bangalore
Custom forgings, made to order.
Gears, valves, rings, shafts, flanges, discs and hubs — forged to your specification in carbon, alloy, stainless and nickel grades.
Products
Parts we manufacture regularly.
Forged to drawing in open and closed die, and finished to whatever stage you need.
How a job runs
From bar stock to a certified component.
Each stage has its own equipment and its own inspection. What follows is what actually happens to your material.
Cutting
Bar and billet are cut to length on band saws and precision cutting machines. Accurate cutting keeps the input weight close to what the part actually needs, which means less material burned off as scrap and a shorter time in the furnace.
Forging
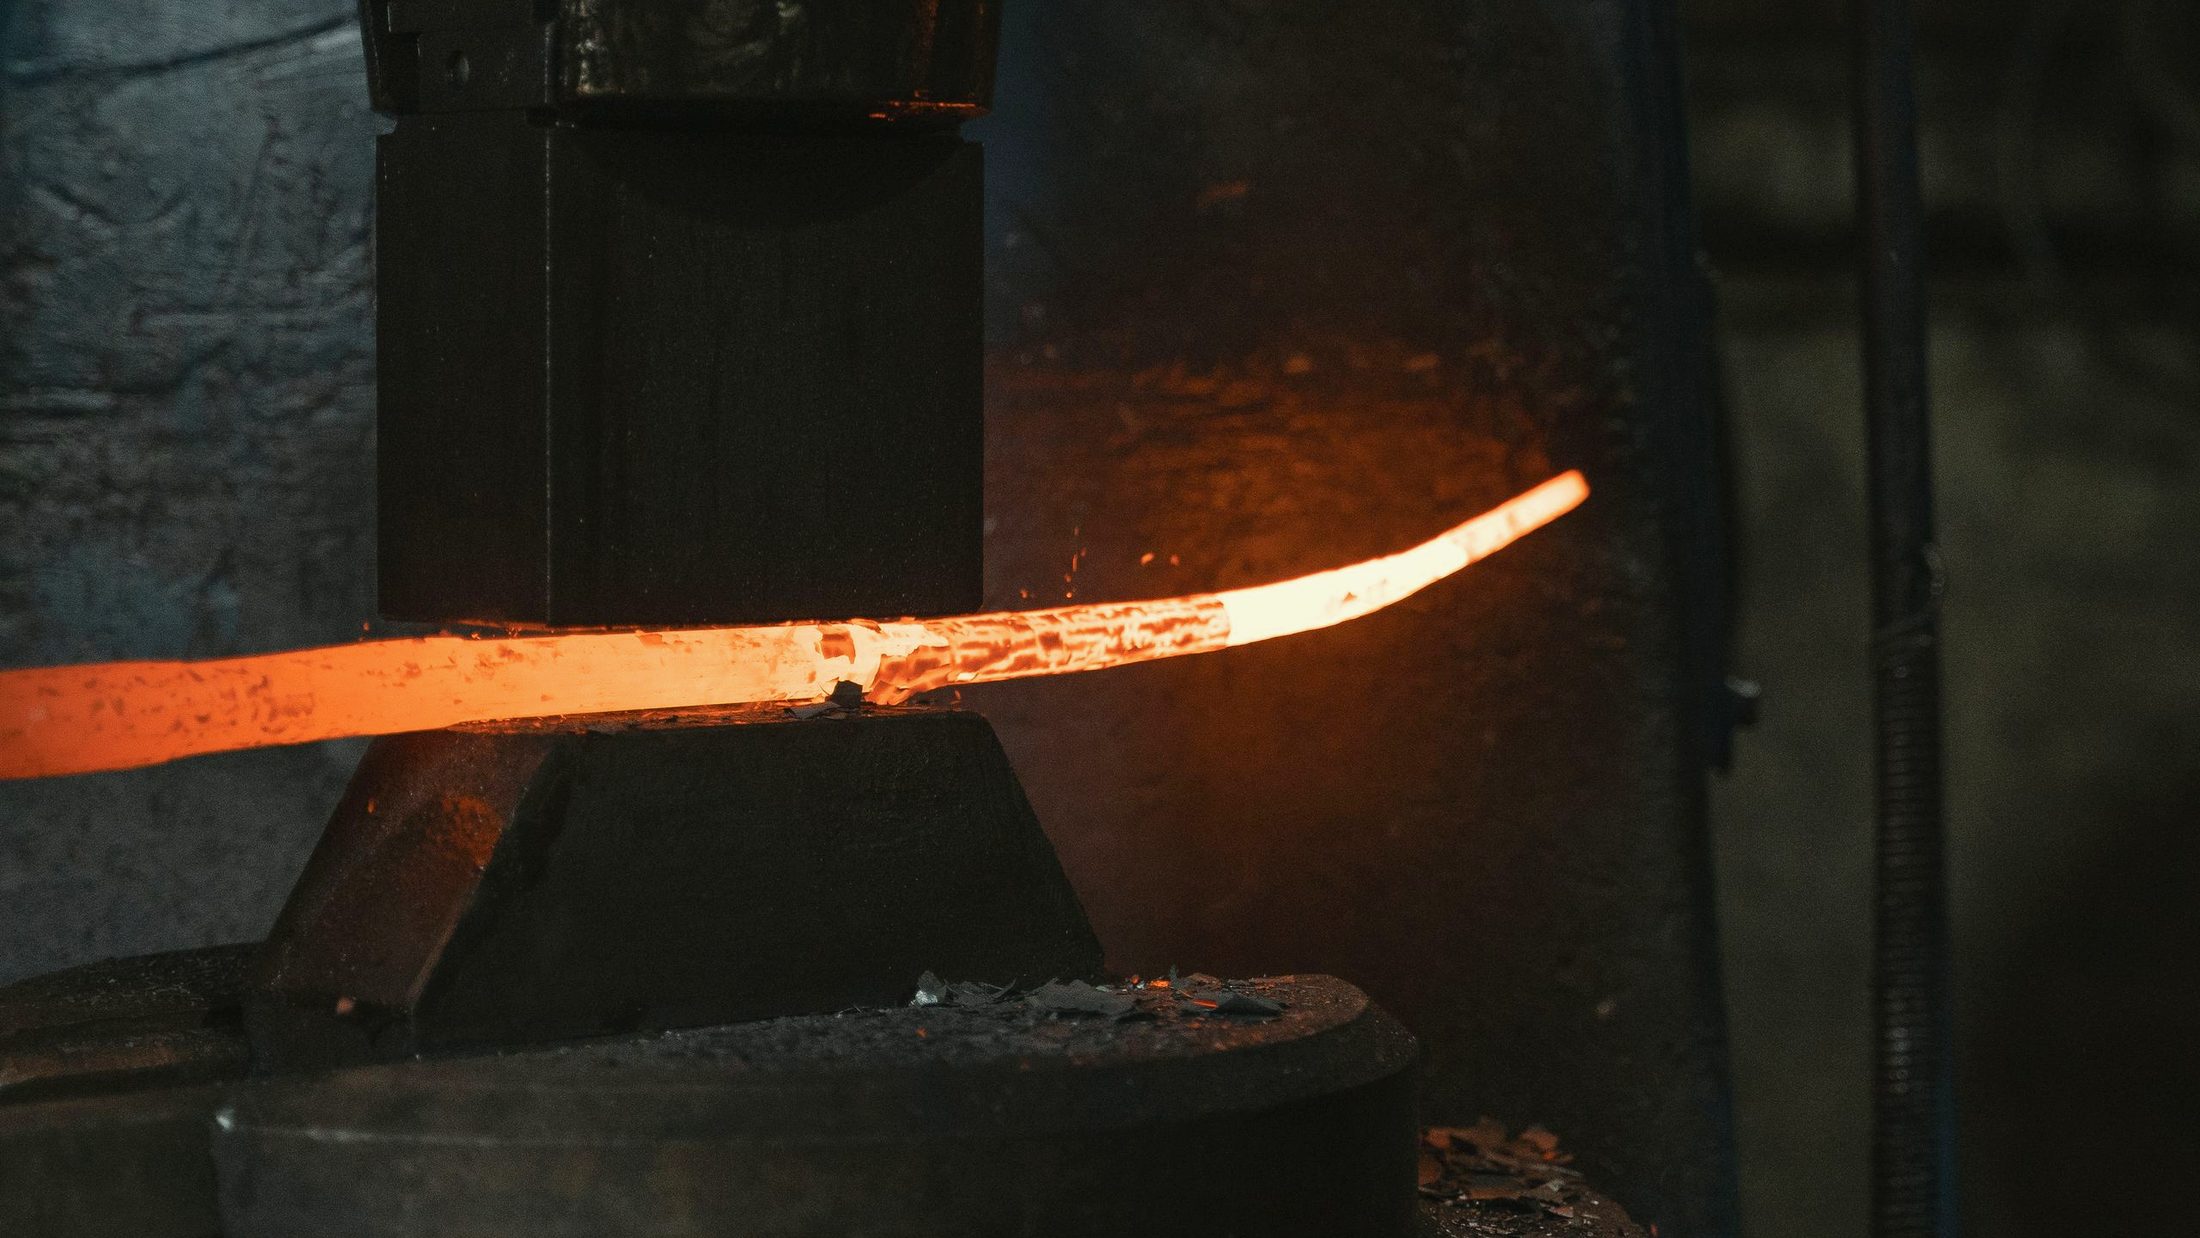
Pneumatic hammers for open die work, where the shape is developed by the operator rather than by tooling. A screw press and a hydraulic press for closed die work that has to repeat. Ring rolling for seamless rings and flanges, which arrive far closer to finished size than a ring machined from solid.
Machining
Vertical turret lathes for discs, rings and flanges; heavy lathes for long shafts between centres; centre lathes for smaller work. Parts leave as forged, proof-machined for your own finishing operations, or turned complete to drawing.
Heat treatment
Handled by our sister concern Rishab Heattreaters, covering case carburizing through to solution annealing. The cycle is matched to the grade and to the properties the drawing calls for, and hardness and case depth are checked on the batch before it moves on.
Quality, at every stage
Material is verified before it is cut, not only after the part is finished. Chemistry is confirmed on the spectrometer and by PMI, hardness is checked after heat treatment, ultrasonic testing finds internal defects before machining time is spent on them, and mechanical properties are proven on test bars. A Material Test Report goes out with the consignment.
Range
Sizes and grades we work in.
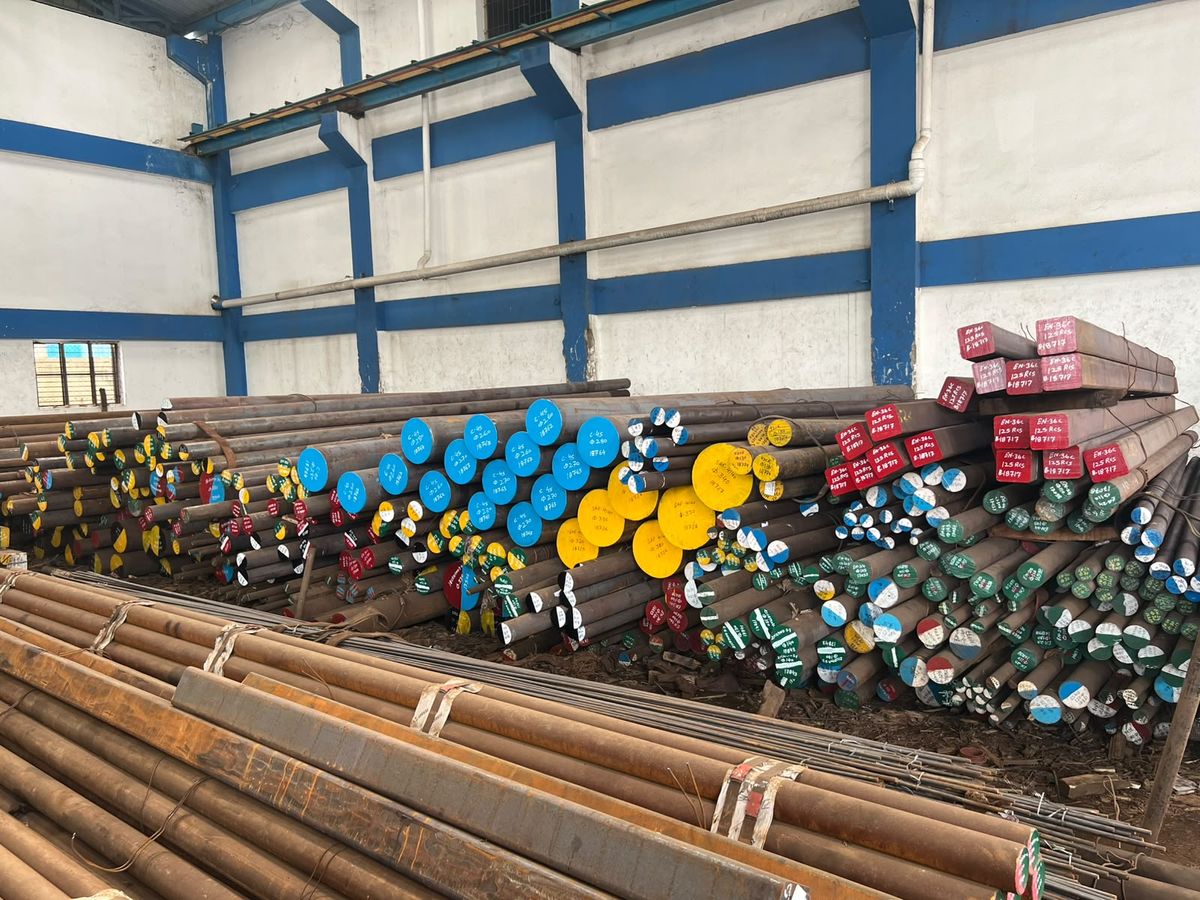
Material comes through Arihant Ispat, our group's stockholding arm, which buys from primary producers and imports where a specification needs it.
| Rounds | Ø18 – 800 mm |
| Flats & squares | 20×20 – 340×400 mm |
| Plates | to 6000 × 2000 × 250 mm |
| Rolled rings | to Ø1500 mm OD |
| Carbon & alloy | EN8, EN19, EN24, EN353, 42CrMo4, 4140, 4340, 8620, 20MnCr5 |
| Stainless & duplex | 304, 316, 410, 420, F51 / 2205, 17-4PH |
| Nickel alloys | Inconel 600, 617, 625, 718 |
Industries
Where these parts are used.
Enquiries
Send us your drawing or specification.
Tell us the part, the grade and the quantity. We confirm whether we can make it, what material it needs, and what it will cost.