Capability
Hammer, press and ring rolling — with the machine shop next door.
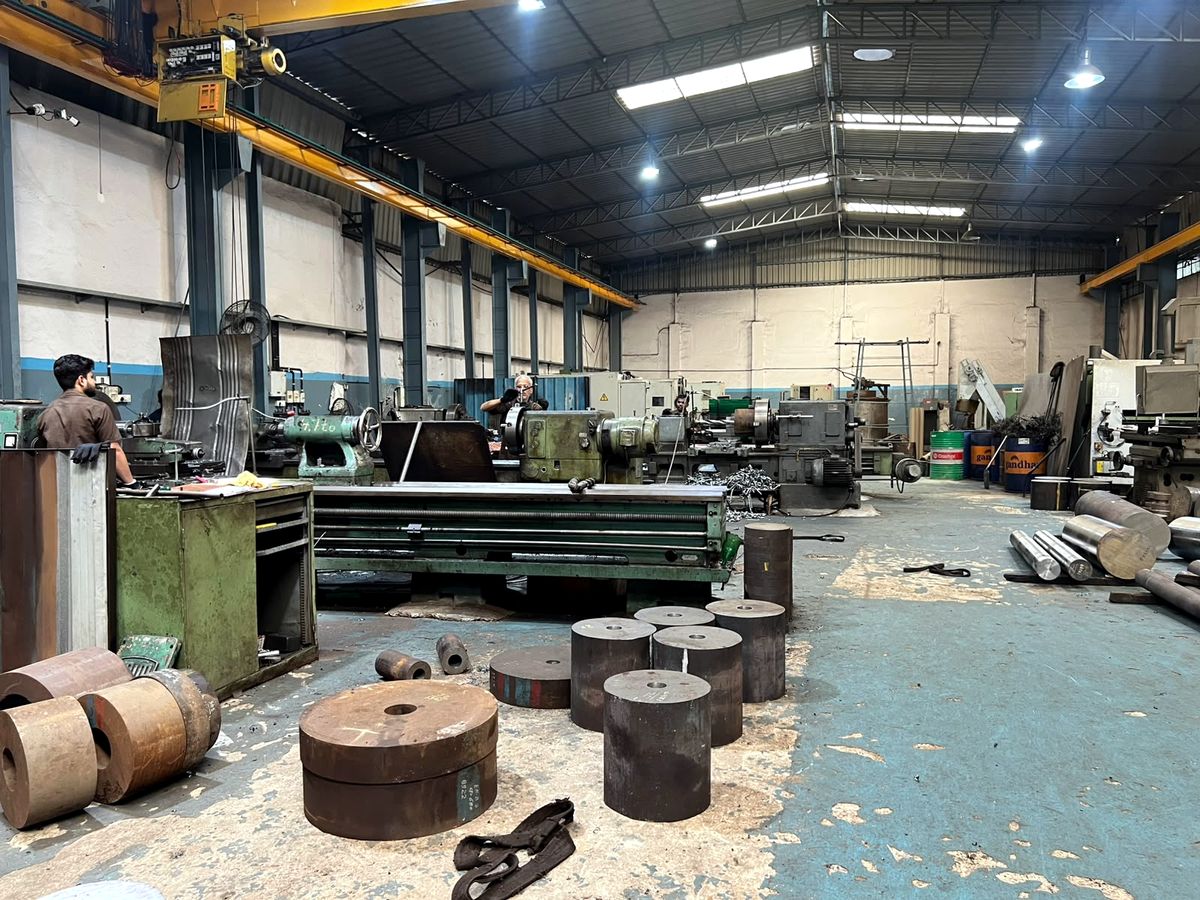
Hammers, presses and ring rolling for the forging; lathes for the finishing; a laboratory to prove it came out right.
2.1 — Forge shop
Open die, closed die and rolled rings.
Hammers where the part is shaped by skill rather than tooling. Presses where it has to repeat. Ring rolling where a seamless ring beats machining one from solid.
| Machine | Capacity / type |
|---|---|
| Beche Pneumatic Hammer | Open die |
| Massey NSE Pneumatic Hammer | Open die |
| KSFPL Screw Press | 200 Tons |
| KSFPL Hydraulic Press | 1200 Tons |
| Ring Rolling — vertical & horizontal | up to Ø1500 mm OD |
| Oil-Fired Pre-heating Furnace | Controlled temperature |
2.2 — Machine shop
Take it black, proof-machined, or ready to fit.
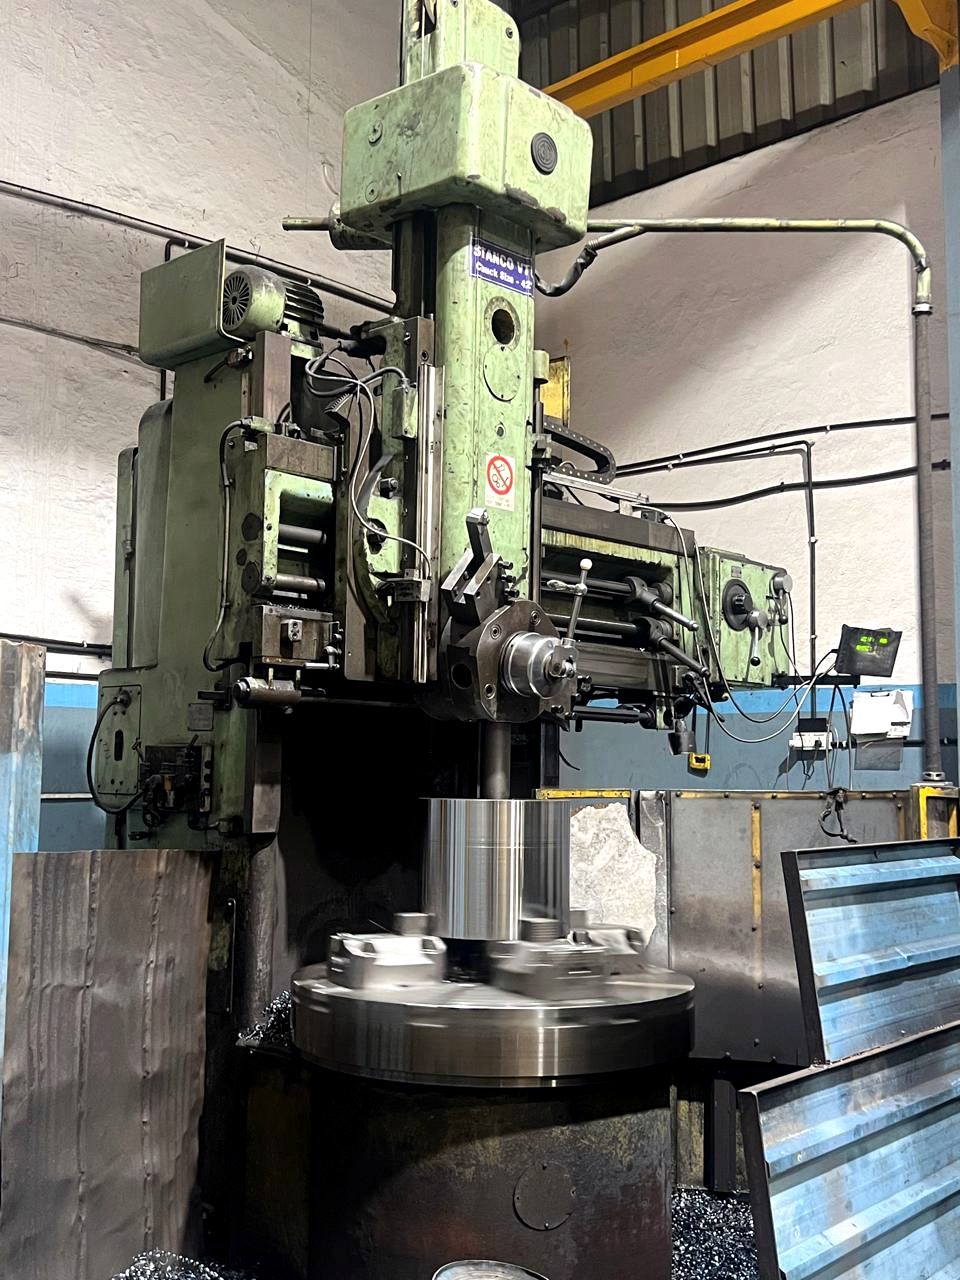
A forging is rarely useful as it comes off the press. Vertical turret lathes, heavy lathes and centre lathes take it to whatever state you want — black, skimmed for inspection, or finished to drawing.
| Machine | Capacity |
|---|---|
| Vertical Turret Lathes (VTL) | up to Ø1300 mm OD |
| Heavy Lathes | up to Ø700 mm OD · 6 m length |
| Centre Lathes | 100 – 600 mm OD |
Upstream — Arihant Ispat
Cut to your length before it reaches the fire.
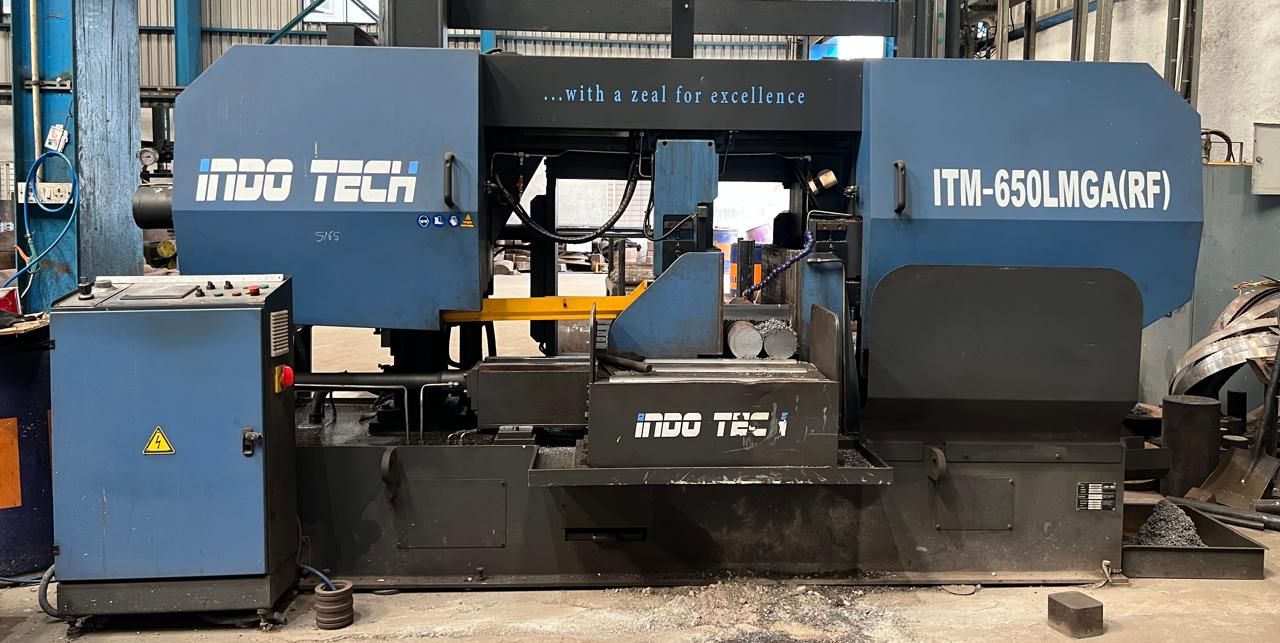
Arihant Ispat cuts sections to size on band saws, up to Ø1250 mm, with flat products slit or cut to your blank size. Nothing goes out for third-party sawing, so the billet is ready the day the order is confirmed.
Downstream — Rishab Heattreaters
Heat treatment, verified before it moves on.
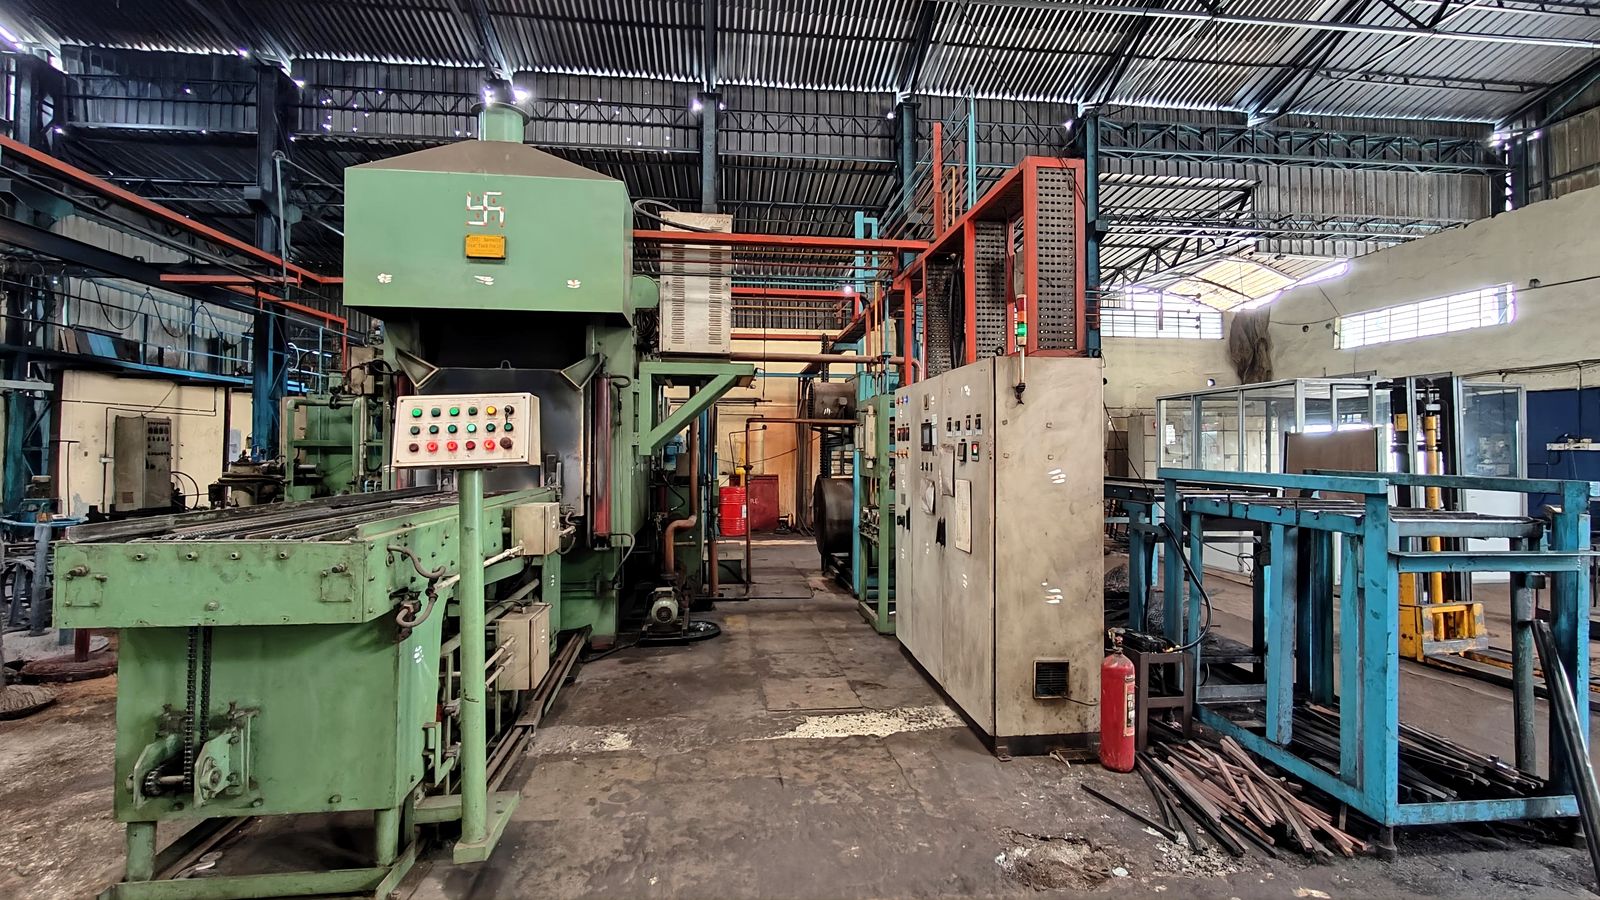
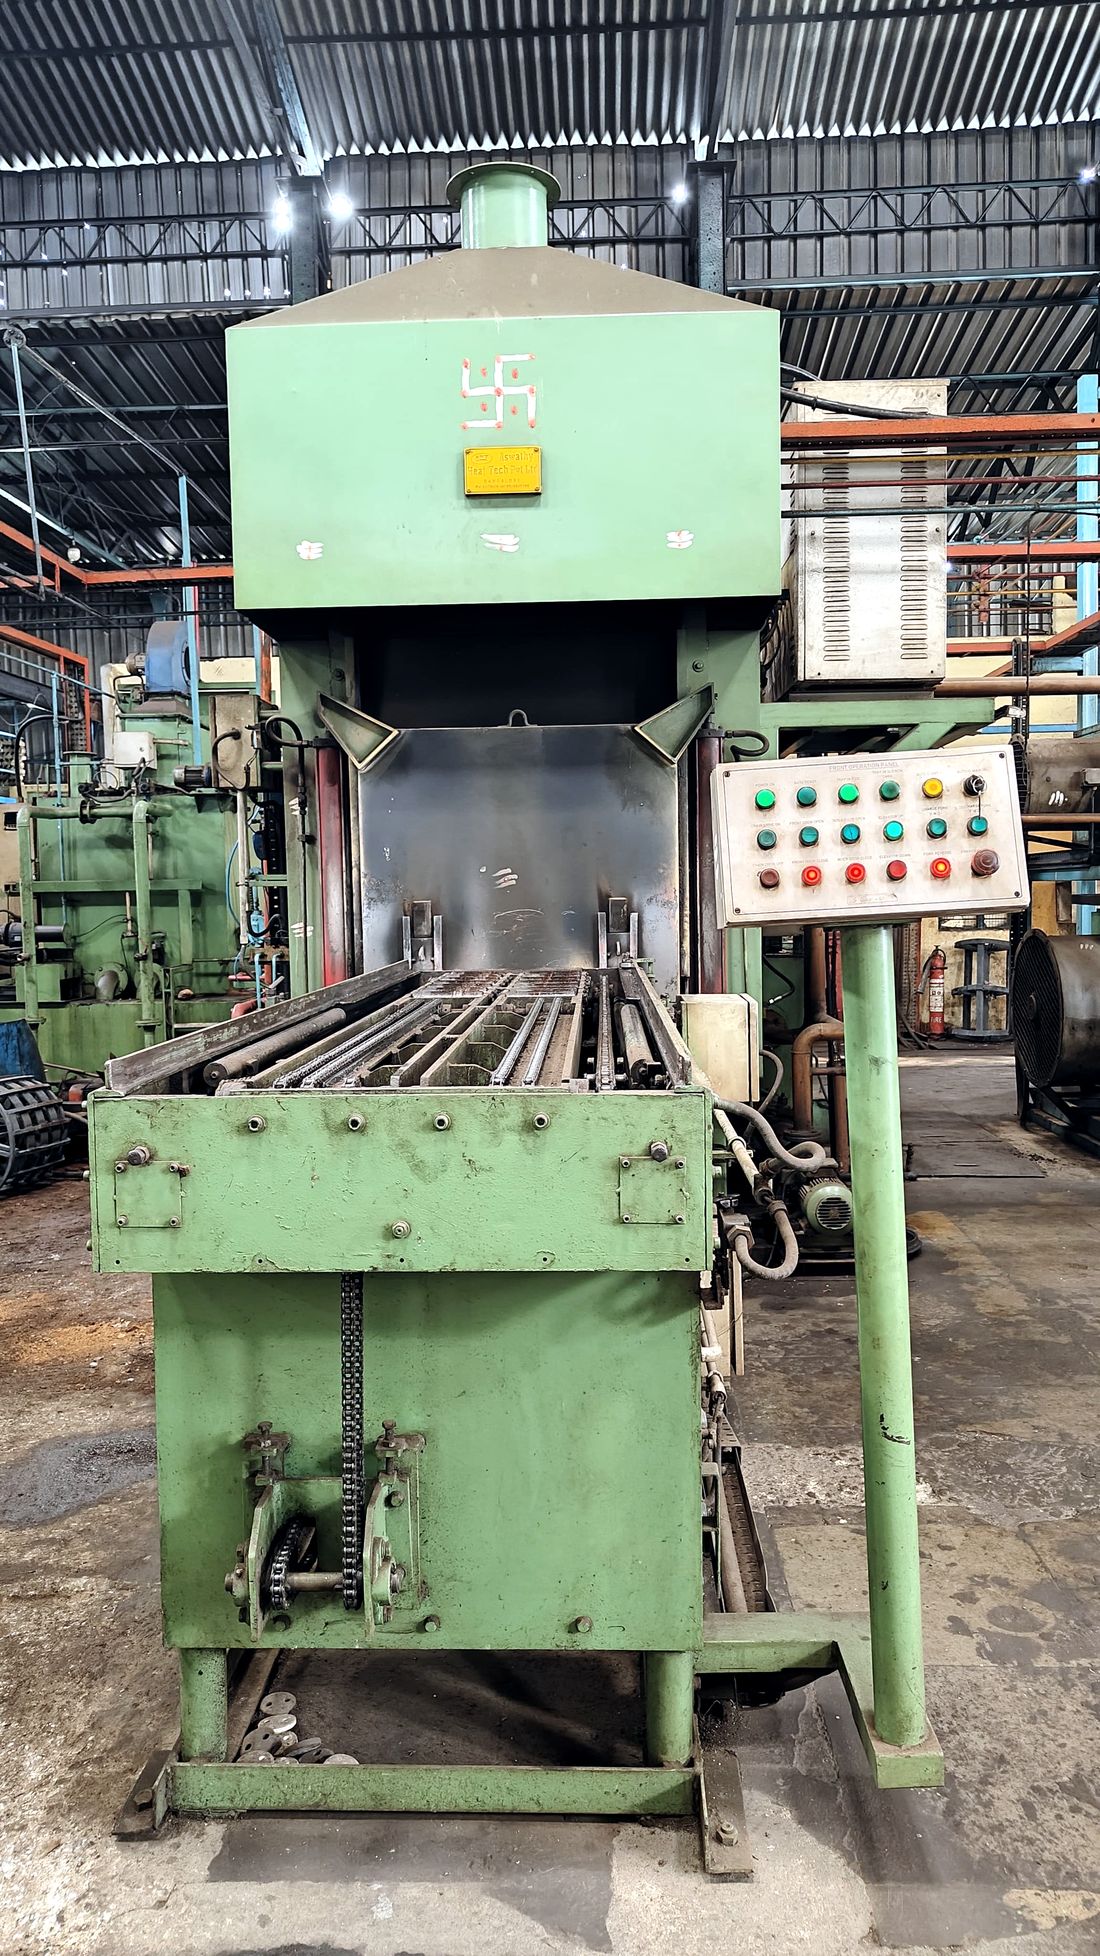
Heat treatment is where a component earns its strength, and where an unverified cycle can hide a failure. Every batch is checked for hardness, case depth and microstructure before it leaves.
| Furnace / plant | Purpose |
|---|---|
| Sealed Quench Furnace | Scale-free case hardening |
| Hardening Furnace | Through hardening |
| Tempering Furnace | Controlled final properties |
| Gas Carburizing Furnace | Deep, uniform case |
| Oil & Water Quench Tanks | Grade-matched quench media |
| Washing Machine | Parts delivered clean |
Next step
Tell us what the part has to do.
Send the drawing or the specification and we will confirm feasibility, material and price.